If you’ve ever stared at a soda can, a cooking pot, or a shiny lid on a takeout container, you’ve held an aluminum circle without even realizing it. I’m the owner of a small aluminum circles supplier, and over the last 12 years, I’ve seen a lot of people ask the same question: “How do you turn a big ol’ slab of aluminum into those perfectly round, thin discs I use for my business?” It’s not some magic trick (promise)—it’s a mix of heavy machinery, tight quality checks, and way more hands-on work than most folks think. Let me break it down like I explain it to my new hires on their first day. Aluminum Circles
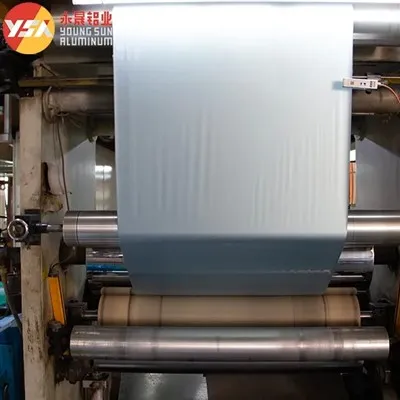
First things first—we don’t just grab a random aluminum block and start cutting. The right base material is everything. Most of the aluminum circles we use for food-grade stuff (pots, can lids, baking sheets) come from AA-grade aluminum alloy, usually 1050, 1060, or 3003. 1050 and 1060 are pure aluminum (99.5%+), which is soft, malleable, and doesn’t react with food. 3003 has a tiny bit of manganese mixed in, making it sturdier for things like cookware that takes a beating. We buy these in huge rolls, not blocks—like, rolls that weigh 10,000 pounds each and are so long you could stretch them out for a mile. That’s our raw input, no shortcuts here.
The first real step is slitting. Those big rolls are way too wide (like 60 inches across) to turn into circles. So we feed them into a slitter machine—think of a giant, precision pair of scissors with sharp, circular blades instead of blades. The machine cuts the wide roll into narrower strips, exactly the width we need for the final circle size. For example, if a customer wants a 10-inch circle, we’ll slit the roll into a strip that’s a little over 10 inches wide (we account for a tiny bit of material loss later). The slitter operator has to be sharp here—if the blades are even a millimeter off, the strips are wonky, and we can’t use them. We also do a quick check here: we run a micrometer over a few strips to make sure the thickness is spot on. Most circles are between 0.2mm and 2mm thick, depending on what they’re for—thin for soda can tops, thicker for a cast-iron skillet base.
Next up is the big one: blanking. This is where those strips become actual circles. We have a blanking press that’s basically a metal stamping machine on steroids. The strip feeds into a die set—two hard steel rings, one on top (the punch) and one on bottom (the die). The punch slams down with like 200 tons of force, cutting a perfect circle out of the strip. It happens so fast—like 10 to 15 strokes per minute—that you barely hear it, just a low thud from the press room. Wait, but why not just cut circles out of a flat sheet instead of strips? Because using rolls of aluminum is way more efficient—less waste, faster production, cheaper for customers. If we used flat sheets, we’d have way more leftover edges that we can’t reuse, but with strips, the leftover offcuts are small enough to melt down and recycle back into new rolls. That’s a big win for both our bottom line and the planet—we recycle almost 90% of our scrap material here.
Blanking is where most of the magic happens, but we can’t just stop there. The freshly cut circles (we call them blanks) are a little rough around the edges—like, sharp burrs from the stamping, and maybe a faint oily coating from the mill we bought the aluminum from. So we send them to a deburring and cleaning station. First, a set of soft, abrasive brushes runs around the edge of each circle to buff away those burrs—no more accidental cuts when a manufacturer handles them. Then, the blanks go through a three-step cleaning process: a alkaline wash to strip away the mill oil, a rinse with pure water, and a dry with hot air. For food-grade circles, we don’t skip this step—even a tiny bit of leftover oil would make a pot smell off or leave a weird taste on a soda can. We also do a spot check here every hour: grab 10 blanks, run a cotton swab over them, and if there’s any discoloration on the swab, we send that batch back for another clean.
Wait, some of you might be thinking—what about circles for decorative stuff, like signage or appliance trim? Those go through a different step after deburring: annealing. Annealing is basically heating the aluminum to make it more flexible, which is great if a customer wants to bend the circle into a curved sign or a decorative dish. We load the blanks into a large annealing oven, heat it to around 500°C (930°F) for a few hours, then let it cool slowly over 12 hours. If we skipped annealing, the aluminum would be too brittle to bend without cracking. For food circles, we usually don’t anneal them—we keep them hard so they don’t warp when you put them on a hot stove. That’s another thing we explain to customers: pick the right alloy and post-processing for what you’re making.
Once the blanks are clean and processed, we move on to sizing and inspection. First, each circle goes through a gauge roller—this makes sure the thickness is consistent across the whole circle, no thin spots that would break when you stamp a lid or bend a handle. Then, we check the diameter with laser sensors. A laser shoots across a spinning circle, and if it’s even 0.1mm too small or too big, it gets rejected. We do 100% of these checks now—way better than the old days where we checked just 1 in 100, and a bad batch would end up back at our dock because a customer’s stamping line broke. We also check for surface defects: tiny scratches, dents, or discoloration. Anything that doesn’t meet our specs gets set aside for recycling—no excuses here, even if a customer says “it’s just for a cheap toy, we don’t care.” Our reputation’s worth more than a few extra circles.
After inspection, we sort the circles by size and grade, then pack them. For most customers, we palletize them on wooden skids, wrap them in plastic to keep them clean, and add shrink wrap so nothing shifts during shipping. For small-batch or custom orders, we box them in corrugated boxes with dividers so the circles don’t scratch each other. We also label every pallet with the alloy, thickness, diameter, and food-safe grade (if applicable)—no guesswork, no mix-ups. Last year, we had a customer mix up a batch of 1050 (pure aluminum) with 3003 (manganese alloy) and try to stamp lids, and the lids cracked. Now we make sure every label is double-checked by two people before it leaves the warehouse.
Now, you might be wondering—why go through all this instead of just casting circles from molten aluminum? Because casting molten aluminum into circles leads to way more defects: air bubbles, uneven thickness, rough edges. Blanking from rolled aluminum is way more precise, faster, and cheaper for high-volume orders. That’s why almost all aluminum circles for industrial use are made this way, not casting. Plus, rolled aluminum is already recyclable—we can melt down scrap blanks, slitter offcuts, and even bad pallets, turn them into new rolls, and start over. It’s a closed loop, which is why our customers love working with us—they know their circles are not just well-made, but eco-friendly too.
I should mention custom orders, because that’s half our business. If you need a weird size—like 18-inch circles for a large baking pan, or super thin 0.1mm circles for battery parts—we can adjust the slitter and blanking press to fit. Last month, a small craft brewery came to us needing 5-inch food-safe circles to make custom bottle caps for their limited-edition IPA. We ran a small batch, checked every one, and delivered them in three days. That’s the thing about being a small supplier—we can’t compete with the big factories on huge bulk orders, but we can bend over backwards for small to medium businesses that need fast turnaround and personalized quality.
A lot of new customers come to us and think aluminum circles are interchangeable, but they’re not. A circle for a soda can can’t be the same as one for a grill cover, and a food-grade one can’t have any chemicals that leach into food. That’s why we’re strict about every step—from picking the right alloy to cleaning the blanks to double-checking dimensions. I’ve had customers tell us, “Your circles are a little more expensive than the other supplier, but they don’t have half the defects.” That’s the stuff that keeps us in business.
So, if you’re a manufacturer needing aluminum circles—for cookware, packaging, decor, whatever—don’t go for the cheapest option. Look for a supplier that walks you through the process, checks quality at every step, and offers customizations. We’re always here to chat through what you need, answer questions, and help you pick the right product for your project.
If you’re tired of dealing with suppliers that cut corners or can’t keep up with your order timelines, hit us up to talk through your needs. We’re ready to make the aluminum circles that work for your business, no hassle, no surprises.
Aluminum Strip Coil References
- Aluminum Association. (2022). Aluminum Rolling and Slitting Process Guidelines.
- American Iron and Steel Institute. (2021). Metal Blanking and Deburring Standards for Food-Grade Applications.
- National Institute of Standards and Technology. (2020). Alloy Selection for Aluminum Circular Components in Consumer Goods.
- World Aluminum. (2023). Sustainable Manufacturing Practices for Aluminum Products.
Henan Yongsheng Aluminum Industry Co., Ltd.
We are one of the most reliable aluminum circles manufacturers and suppliers in China. With abundant experience, we warmly welcome you to buy high-grade aluminum circles for sale here from our factory. All custom made products are with high quality and competitive price.
Address: Gongyi City Industrial Cluster District, Huiguo Town, Gongyi City, Henan Province
E-mail: eric@ysaluminum.cn
WebSite: https://www.ysaluminummill.com/
